When it comes to packaging options, Barrier Pouches have really become a hot topic in terms of quality and efficiency. I remember reading what Dr. Emily Chen, a well-respected expert at Packaging Innovations, once said—she mentioned that the way these pouches protect their contents is absolutely crucial for keeping food fresh and safe. That really sums up how important they are across different industries, whether it’s food, pharma, or others.
These pouches are built tough, designed to handle all sorts of environmental challenges. They offer solid protection against moisture, oxygen, and light—so your products stay as they should. But, let’s be honest, it’s not all smooth sailing in the market. Some manufacturers still find it tricky to keep up with the growing push for sustainability and better functionality. It’s pretty clear that innovation’s the way forward, but quality can’t get lost in the process.
Also, understanding what customers actually need is super important. Every industry has its own special requirements for Barrier Pouches, and chatting regularly with clients can reveal some valuable insights that help improve the product. As we keep exploring this packaging world, it’s key to stay aware of how things are always changing. Striving for excellence in Barrier Pouches? Totally worth the effort—it’s a journey we’re all on together.
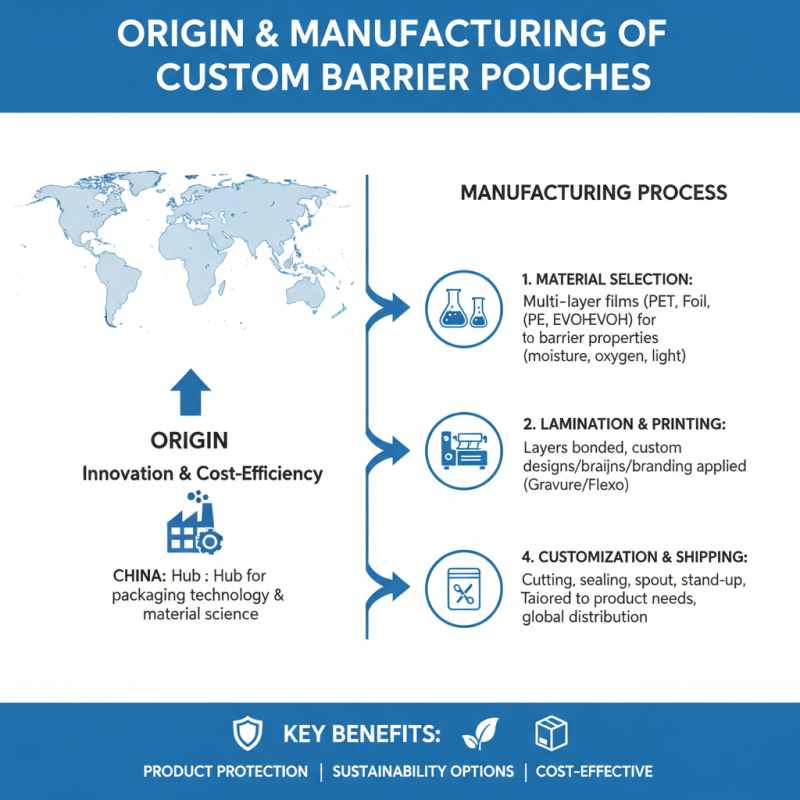
Origin and Manufacturing Process of Custom China Barrier Pouches
Custom China barrier pouches have become essential in various industries. These pouches offer superior protection for sensitive products. Understanding their origin and manufacturing process is crucial for businesses seeking quality packaging solutions.
The manufacturing process begins with raw materials such as multi-layer films. These materials are chosen for their barrier properties. Once the materials are ready, specialized machines create the pouches. The process involves precise cutting, sealing, and printing. Attention to detail is necessary to ensure the final product meets industry standards. However, errors can occur, leading to discrepancies in quality. Continuous improvement in production techniques is vital.
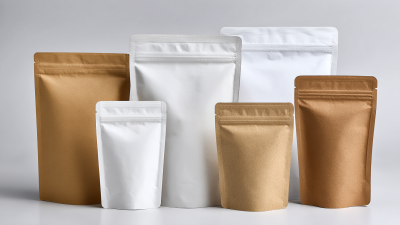
Stand Up Barrier Pouches are designed for convenience. They allow easy display and storage. Yet, companies may overlook the importance of proper testing. Rigorous quality control measures can prevent potential failures. By focusing on the right manufacturing practices, businesses can ensure reliability and protect their products effectively.
Key Materials Used in Quality Barrier Pouch Production
When it comes to packaging solutions, quality is paramount. Barrier pouch production relies heavily on specific materials that enhance the integrity of the packaging. Commonly used materials include polyethylene, aluminum foil, and specialty films. Each material serves a distinct purpose, such as protecting contents from moisture, oxygen, or light. These factors are crucial in preserving the freshness and potency of products.
Perfecting Barrier Bags starts with selecting the right materials. For example, metallic films offer superior barrier properties, making them ideal for food packaging. Customers often seek pouches that can resist punctures and tears. However, striking a balance between flexibility and durability can be challenging. It is vital to assess each material’s performance under different conditions.
Tip: Always test barrier bags with your product to ensure compatibility. An effective seal is essential in ensuring the longevity of your items. Pay attention to the pouch's closure mechanism; it can significantly impact container integrity. Choose materials that align with your environmental goals. Many companies now prioritize recyclable options and sustainable resources. This is a crucial consideration for brand reputation and marketability.
Market Trends: Demand for Customized Barrier Pouches in Packaging
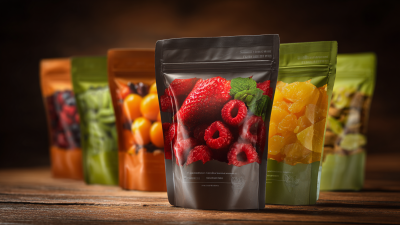
The demand for customized Barrier Pouches is rising significantly. Businesses are increasingly realizing the importance of effective packaging solutions. These pouches provide strong protection against moisture, oxygen, and light. This is critical for preserving product quality, especially in food and pharmaceuticals.
More companies are exploring personalized designs. Customization allows brands to stand out in a crowded market. Clients seek unique sizes, colors, and printing options. This adds to the visual appeal of their products. However, finding the right supplier can be a challenge. The market is filled with options, but not all are reliable.
It’s essential to evaluate suppliers carefully. Quality control must be a priority. Some companies may offer lower prices but compromise on quality. This can lead to spoilage, loss of freshness, and ultimately, customer dissatisfaction. Investing in reliable barrier pouches is crucial for maintaining a brand's reputation and ensuring product integrity. Thoughtful choices in packaging reflect a brand's commitment to excellence.
Market Trends: Demand for Customized Barrier Pouches in Packaging
Comparative Analysis: Custom Barrier Pouches vs. Traditional Packaging Solutions
In recent years, custom barrier pouches have emerged as an effective alternative to traditional packaging solutions. These pouches are designed with multi-layer structures that provide superior moisture and oxygen barrier properties. This is essential for preserving product freshness and extending shelf life. Unlike standard packaging, barrier pouches can be tailored to meet specific needs, such as size, print durability, and seal strength.
While traditional packaging often relies on single material types, barrier pouches combine different materials for enhanced performance. Many companies find that custom barrier pouches also reduce material waste, which is a growing concern in sustainable practices. However, the initial cost of these pouches can be higher compared to conventional options. This investment raises questions about long-term savings in product loss and spoilage.
Businesses must weigh the benefits of custom barrier pouches against their budget constraints. Not every product may require advanced barriers. There can be a learning curve in transitioning from traditional packaging to barrier pouches. Ensuring that staff are trained correctly is vital to avoid mistakes and waste. Overall, understanding these factors can lead to better packaging choices and improved product protection.
Quality Standards and Certifications for Barrier Packaging in the Industry
Quality standards and certifications are crucial in the barrier packaging industry. These criteria ensure that materials can withstand various environmental factors. For instance, effective moisture resistance is vital for preserving the integrity of sensitive products. Companies might struggle to find suppliers that consistently meet these standards. This inconsistency can lead to problems in product safety and shelf life.
In the realm of barrier packaging, certain certifications hold significant weight. ISO certifications demonstrate a commitment to quality management. Additionally, compliance with FDA regulations plays a key role for food packaging. These certifications build trust with customers and provide assurance of product safety. However, not all suppliers prioritize obtaining these credentials. This creates challenges for businesses that rely on quality materials.
Many manufacturers overlook the importance of regular audits. These checks ensure that packaging consistently meets industry standards. Neglecting them can lead to failures in product safety or performance. Companies must stay vigilant and regularly assess their packaging processes. While striving for high standards, reflections on these practices can lead to better outcomes in the long run.
Custom China Barrier Pouches Supplier for Quality Packaging Solutions - Quality Standards and Certifications for Barrier Packaging in the Industry
| Dimension |
Material Type |
Barrier Properties |
Certifications |
Applications |
| 300mm x 400mm |
PET/AL/PE |
Oxygen Barrier 0.1 cc/m²/day |
ISO 9001, BRC |
Food Packaging |
| 250mm x 350mm |
NY/Nylon |
Moisture Barrier 0.05 gm/m²/day |
FDA, SGS |
Pharmaceuticals |
| 200mm x 300mm |
CPP |
Light Barrier 0.3 lux hours |
ISO 22000, HACCP |
Cosmetics |
| 400mm x 500mm |
PET/PE |
Chemical Resistance |
RoHS, REACH |
Industrial Chemicals |
Innovative Technologies in the Production of Barrier Pouches
In recent years, innovative technologies have transformed the production of barrier pouches, a crucial aspect of
Barrier Packaging.
These pouches are essential for preserving product freshness and extending shelf life. Advanced materials, such as
multilayer films, enhance the barrier properties against moisture, oxygen, and light.
According to a recent industry report by Smithers Pira, the global barrier packaging market is expected to reach
$41 billion by 2026, highlighting the demand for high-quality packaging solutions.
One significant breakthrough in barrier pouch technology is the development of biodegradable materials.
This innovation addresses environmental concerns and consumer preferences. Manufacturers are increasingly exploring options that reduce plastic waste while maintaining functionality.
However, not all biodegradable materials perform equally. Some may require specific conditions to break down effectively, leading to doubts about their overall reliability in long-term preservation.
Tips: Always evaluate the material's properties before choosing barrier packaging.
Consider factors such as product type and storage conditions. Regularly review advancements in packaging technologies to stay informed on the best options.
Embracing innovative solutions may seem daunting, but it can lead to better product performance and customer satisfaction.
Balancing durability, sustainability, and cost is a continual challenge for manufacturers.
Case Studies: Successful Implementation of Barrier Pouches Across Sectors
Barrier pouches offer significant advantages across multiple sectors. Their ability to keep products fresh and safe makes them a top choice for various applications. For example, in the food industry, they prevent moisture and oxygen from compromising quality. In pharmaceuticals, they protect sensitive medications from environmental factors. This versatility demonstrates their importance in quality packaging solutions.
Implementing barrier pouches requires careful consideration. Companies often face challenges in material selection and design. The right materials must align with product specifications. Custom designs can enhance functionality but may also lead to higher costs. It's essential to evaluate these factors before moving forward.
Tips: Always conduct a pilot test when introducing barrier pouches. This helps identify potential issues early on. Collaborate with suppliers who understand your industry needs. Regular feedback loops can drive improvements in design and performance. It's about finding the right balance between cost and quality while ensuring effective packaging solutions.
Innovative High-Barrier Plastic Solutions for NFC Juice: Explore Huadi's Customizable 20L and 25L Bag-in-Box Options
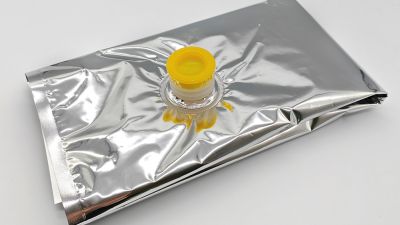
High-barrier Bag-in-Box (BIB) packaging represents a groundbreaking advancement in preserving the integrity of sensitive products such as NFC (Not From Concentrate) juice. This innovative solution is designed to combat the detrimental effects of external factors including oxygen, moisture, and light—all of which can significantly compromise the quality and shelf-life of juice products. By combining a flexible inner bag with a robust outer box, the BIB system provides an effective barrier that ensures optimal freshness and extends the product’s usability.
One of the standout features of high-barrier BIB packaging is its customizable options, particularly in sizes like 20L and 25L. This flexibility allows businesses to tailor their packaging solutions to meet the specific needs of their product lines. The design not only enhances convenience for storage and transport but also ensures the juice remains uncontaminated until it is ready for consumption. Additionally, this packaging solution supports sustainability efforts by optimizing the use of materials, thus reducing waste while maintaining high standards of quality and safety.
In conclusion, high-barrier Bag-in-Box packaging epitomizes a modern approach to preserving juice products, providing both functional advantages and environmental benefits. Brands looking to enhance their product offering can greatly benefit from adopting this innovative packaging solution that caters to the demands of today’s consumers.
FAQS
: Custom barrier pouches provide excellent protection for sensitive products. They are used in various industries.
Multi-layer films are the primary materials. They are chosen for their effective barrier properties.
The manufacturing involves cutting, sealing, and printing. Specialized machines ensure precision in the process.
Errors can happen, causing quality discrepancies. Continuous improvement in manufacturing techniques is necessary.
They prevent moisture and oxygen from affecting food quality. This keeps products fresh for longer.
They protect sensitive medications from environmental factors. This helps in maintaining their efficacy.
Material selection and design considerations can be tricky. Custom designs may increase costs as well.
Conduct a pilot test to identify potential issues. Early detection can save costs and time.
Collaborate with knowledgeable suppliers for better insights. Regular feedback loops can enhance design performance.
Find a balance between cost and quality. It’s essential for effective packaging solutions.
Conclusion
The article delves into the significance of custom China barrier pouches, highlighting their origin and the manufacturing processes involved in creating high-quality packaging solutions. The discussion encompasses the key materials essential for producing effective barrier pouches, as well as the rising market trends that show an increasing demand for customized packaging options. Furthermore, it presents a comparative analysis between custom barrier pouches and traditional packaging solutions, emphasizing the unique advantages that barrier pouches offer.
Additionally, the article examines the stringent quality standards and certifications required within the industry, ensuring that barrier packaging meets the highest safety and performance criteria. Innovations in technology are also explored, showcasing advancements in the production of barrier pouches. Finally, the article includes case studies that illustrate the successful implementation of barrier pouches across various sectors, demonstrating their versatility and effectiveness in contemporary packaging solutions.