


How to Choose a Custom Bag in Box Manufacturer for Liquid Packaging
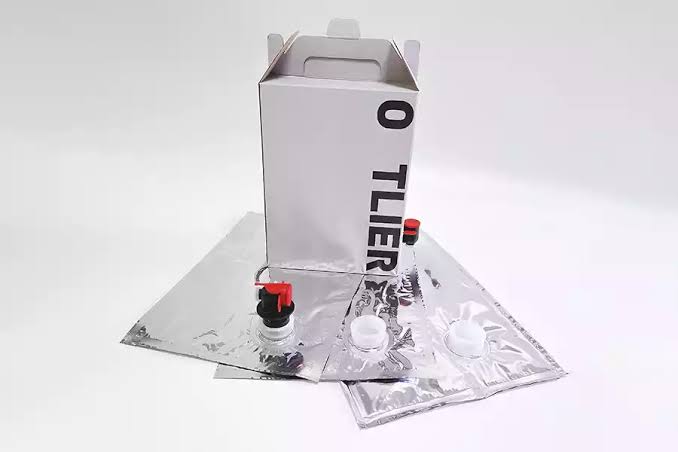
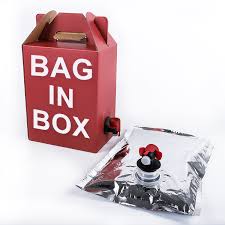
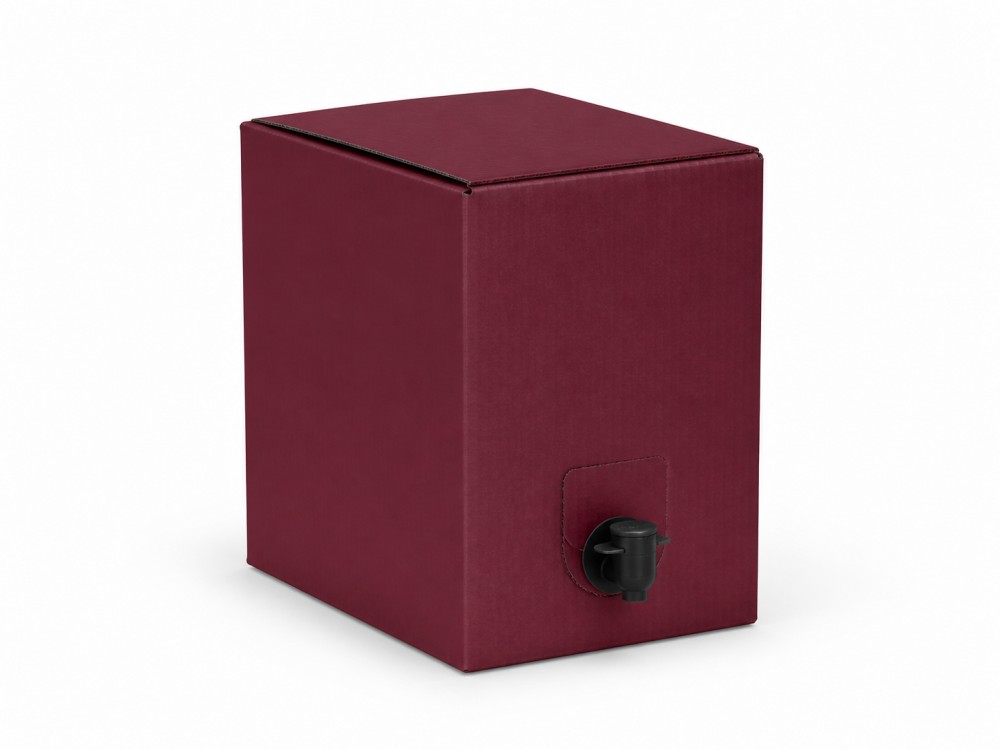
A bag-in-Box Package looks simple from the outside, but its performance depends on a connected system: the liquid, flexible film, seals, fitment, tap or cap, carton, filling process, distribution route, and expected shelf life. A supplier that treats these elements as separate commodities may produce a bag that passes a visual inspection yet fails during filling, transport, dispensing, or storage.
Choosing a custom bag in box manufacturer therefore requires more than comparing unit prices and sample appearance. Buyers need evidence that the proposed structure is compatible with their product, can run on the intended filling equipment, and can be reproduced under controlled production conditions.
Define the Liquid Before Discussing the Bag
Start with product chemistry and handling conditions. Identify whether the liquid is water-based, oily, acidic, alkaline, alcoholic, dairy-based, oxygen-sensitive, particulate, or chemically active. Provide viscosity, pH, alcohol content, oil content, filling temperature, treatment method, and any ingredients that may migrate into or extract substances from the packaging.
Use the actual formulation for compatibility work
A generic description such as “juice” or “detergent” is not enough when flavors, preservatives, surfactants, solvents, or essential oils vary by formulation. Representative product contact testing gives a more reliable basis for film and fitment selection.

Translate Shelf-Life Goals into Barrier Requirements
Oxygen, water vapor, aroma, light, and external contamination affect liquids differently. Wine and juice may need strong oxygen control; edible oil may require oxygen and light protection; water may prioritize taste neutrality and seal integrity. State the target shelf life, storage temperature, exposure to light, and expected time after opening.
Barrier performance belongs to the complete laminate and closure system. A high-barrier film cannot compensate for oxygen entering through an unsuitable tap, poor weld, or excessive headspace.
Ask for measurable properties
Where performance is critical, request film structure, thickness, oxygen-transmission and water-vapor-transmission data under stated test conditions. The values should relate to the converted bag, not only to an unprocessed film data sheet.
Select the Film Structure Around Risk
PE, PP, metallized layers, aluminum-coated structures, and multi-layer composite films offer different sealing, toughness, barrier, stiffness, temperature, and recycling characteristics. The correct choice follows the liquid and supply chain rather than a default layer count.
- Confirm the product-contact layer and its food-contact or chemical-compatibility role.
- Define total thickness and permitted variation.
- Review flex-crack resistance for folded and transported bags.
- Identify whether light barrier or product visibility is more important.
- Check sealing behavior at the intended filling and handling temperatures.
Huadi presents PE, PP, and multi-layer composite options with adjustable thickness and barrier performance across capacities from 1L to 220L. A buyer should convert these options into a product-specific specification before approval.
Treat the Valve and Fitment as Part of the Package
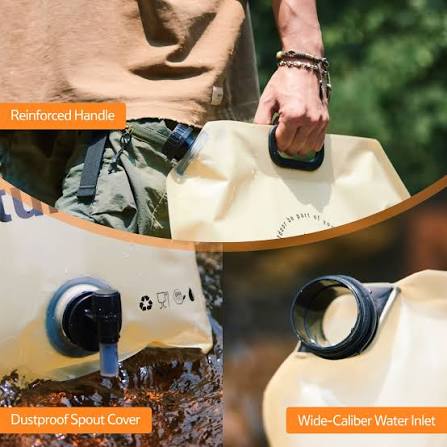
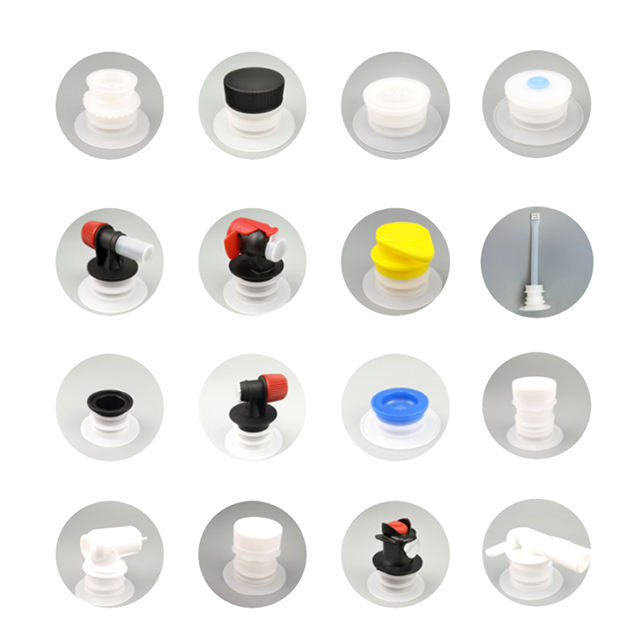
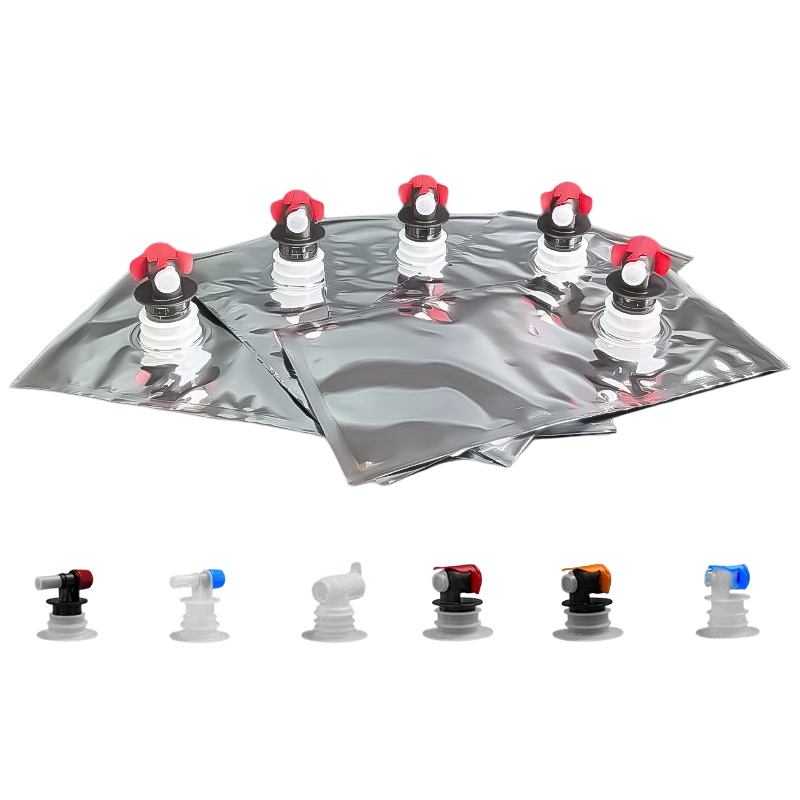
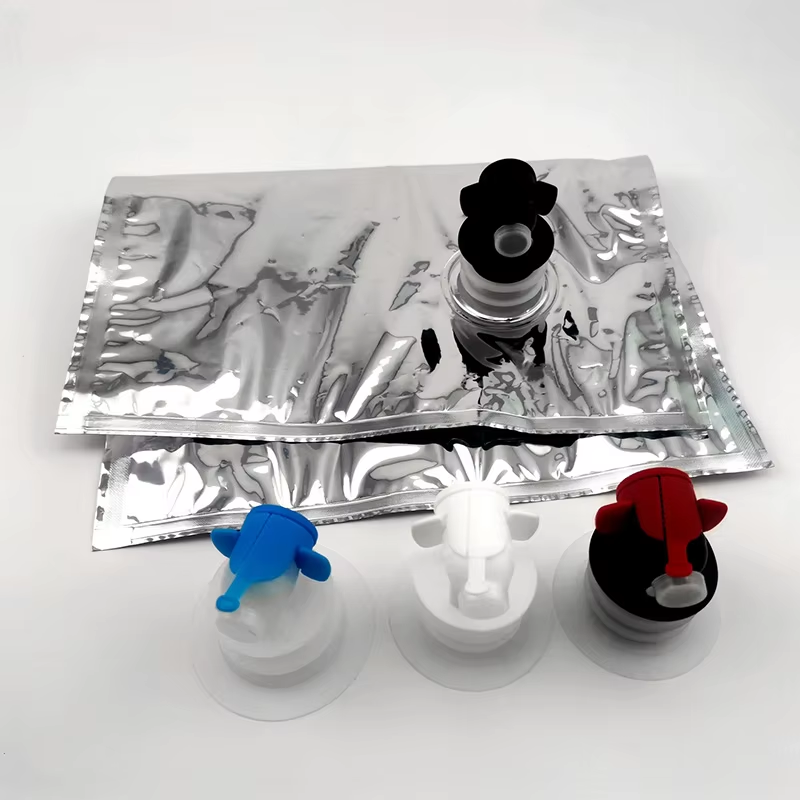
The fitment affects filling speed, dispensing, residual product, oxygen entry, tamper evidence, and compatibility with the outer carton. Specify neck diameter, flange design, closure type, flow requirement, opening force, reclosure behavior, and connection to filling equipment.
Match the closure to product viscosity and use
A free-flowing beverage, viscous syrup, edible oil, and industrial liquid do not dispense in the same way. Flow path, venting behavior, tap design, and user orientation should be tested with the actual product rather than judged from water trials alone.
Check Filling-Line Compatibility Early
Provide the filling-machine model, chuck or connector details, filling direction, line speed, fill temperature, target volume, headspace, and whether the process is manual, semi-automatic, automatic, hot-fill, or aseptic. Small differences in fitment dimensions or film stiffness can affect loading, sealing, and cycle time.
A production-intent line trial should verify bag presentation, fitment engagement, fill accuracy, seal condition, handling, and carton insertion. It is less expensive to adjust a sample than to discover incompatibility after printed inventory is produced.
Define Capacity by Usable Fill, Not Nominal Size
A nominal 10L bag does not automatically provide the correct headspace, carton fit, or dispensing behavior for every liquid. Density, foaming, filling accuracy, product expansion, bag dimensions, and carton geometry influence usable capacity.
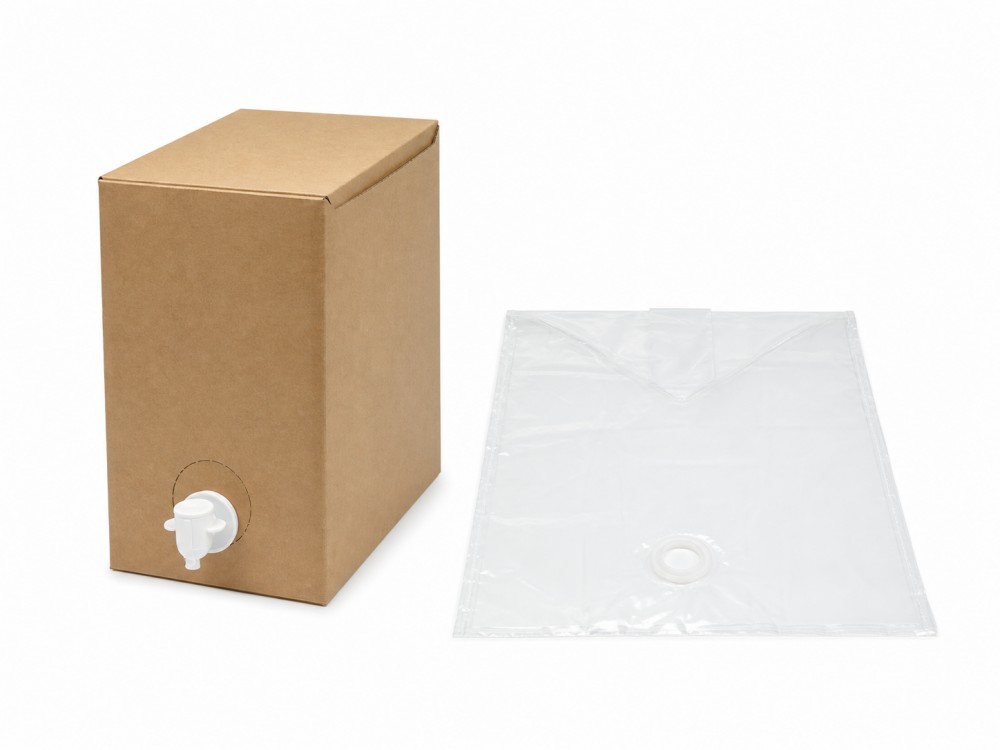
Coordinate bag and carton dimensions
An oversized bag may fold unpredictably or become trapped during dispensing. An undersized bag may move excessively and load the fitment. Approve the inner bag and outer box as a matched system using the intended fill volume.
Build Printing and Artwork into Engineering Review
Printing communicates brand and handling information, but inks, registration, cure, laminate sequence, and artwork location must not interfere with sealing or inspection. Define colors, print method, orientation, code area, regulatory text, and protected zones around seals and fitments.
Approve both digital artwork and a physical color or print sample. The approval record should identify the current revision so obsolete graphics cannot reappear during a repeat order.
Evaluate the Manufacturer Through Process Control
A useful factory review follows the package through material receiving, printing, lamination, curing, cutting, bag making, fitment assembly, inspection, packing, and release. Huadi lists this sequence on its website and states that it operates multiple production lines for liquid and Food Packaging.
Equipment quantity alone does not prove control. Ask how film lots, inks, adhesives, fitments, machine settings, operators, inspection results, and finished batches are traced. The response should show how the factory prevents mixing and reacts to abnormal results.
Connect certification claims to the quoted product
Huadi states ISO 9001 and FDA-related food-packaging compliance and references EU and US food-contact requirements. Buyers should request current, scope-appropriate documents and confirm which materials, manufacturing sites, and finished-package applications they cover.
Use a Structured Supplier Comparison
Supplier evaluation becomes clearer when every candidate answers the same application-specific questions. The comparison should emphasize evidence and manufacturing fit instead of relying on broad statements such as “food grade,” “high barrier,” or “leak proof.”
A concise decision matrix can separate what must be confirmed at quotation, sampling, and production approval. Commercial terms belong in the review, but they should not replace technical validation.
| Review area | Evidence to request | Sample-stage check | Production control |
| Liquid fit | Compatibility and barrier rationale | Actual-product fill trial | Approved film and fitment lots |
| Filling line | Fitment drawing and machine match | Production-speed line trial | Setup limits and first-piece approval |
| Seal integrity | Seal method and test conditions | Leak, pressure, and handling tests | In-process seal and leak checks |
| Printing | Artwork and ink specification | Printed sample approval | Revision and color controls |
| Supply | Lead time and capacity basis | Pilot order performance | Traceability and change notification |
The matrix keeps commercial comparison tied to application evidence. Final approval still depends on the actual liquid, filling process, distribution route, and agreed acceptance limits. Approve Samples in Deliberate Stages
Begin with unprinted prototypes to evaluate dimensions, film behavior, fitment, filling, carton fit, and dispensing. Move to printed samples only after the structure is stable. Production-intent samples should use the approved materials, equipment route, closures, artwork, and inspection methods.
- Record sample construction and material lot.
- Fill with the actual product under representative conditions.
- Condition samples at expected storage temperatures.
- Test handling, drop, vibration, stacking, and dispensing as applicable.
- Inspect seals, folds, fitments, and product contact after testing.
- Keep approved samples and reports linked to the drawing revision.
Define Quality Tests and Acceptance Criteria
A vague requirement for “no leakage” does not explain test pressure, duration, sample conditioning, orientation, or failure criteria. The control plan may include dimensional inspection, seal-width review, seal-strength testing, leak or pressure testing, burst testing, drop testing, fitment pull or torque checks, visual inspection, and migration or compatibility evidence.
Test the weakest realistic condition
Seals may behave differently immediately after production, after curing, at low temperature, or after flexing in transport. Validation should include the conditions most likely to challenge the film, seal, and fitment rather than only an easy room-temperature check.
Examine Logistics and Packed Efficiency
Flexible inner bags can reduce empty-package volume, but folded shape, carton quantity, pallet pattern, humidity protection, fitment protection, and labeling determine real logistics performance. Confirm whether bags arrive individually separated, stacked, bagged, or packed for automated feeding.
Transit trials should use production packaging and the expected route. A package that survives local handling may behave differently during container transport, temperature cycling, prolonged stacking, or repeated transfers.
Compare Cost at the Filled-Pack Level
The lowest bag price may create higher costs through filling interruptions, leakage, excessive product residue, carton damage, slow dispensing, or rejected inventory. Compare film, fitment, printing, carton, filling efficiency, freight, storage, yield, and failure risk at the complete-pack level.
Ask suppliers to state assumptions behind their quotation: material structure, thickness, closure, printing coverage, order quantity, testing, packaging, tooling, freight terms, and revision. Comparable quotations require comparable specifications.
Control Changes After Approval
Material suppliers, film layers, thickness, adhesive, ink, fitment resin, dimensions, equipment, sealing settings, and subcontracted processes can affect performance. Define which changes require notification, samples, documents, or revalidation before production.
Preserve a reproducible golden baseline
The approved record should include drawings, film and fitment specifications, artwork, samples, test results, packing method, and authorized deviations. Repeat orders should reference this baseline instead of relying on memory or an old purchase description.
Conclusion
A reliable custom bag in box manufacturer combines application engineering with controlled conversion. Buyers obtain stronger results when they define the liquid, shelf life, film, fitment, filling line, capacity, printing, tests, logistics, and change rules as One Packaging system. Careful sample validation and documented production controls protect both product integrity and long-term supply consistency.
FAQ
These questions address the decisions buyers most often face when developing customized Liquid Packaging.
What information is needed for a custom bag-in-box quotation?
Provide liquid type and formulation, capacity, annual and order volume, shelf life, filling method and temperature, film or barrier needs, fitment, printing, carton dimensions, tests, certifications, packing, and destination.
Which film is best for bag-in-Box Packaging?
There is no universal best film. Selection depends on product chemistry, oxygen and moisture sensitivity, light exposure, sealing conditions, flexing, storage, shelf life, compliance, and sustainability goals.
How should a bag-in-box valve be selected?
Match the valve to product viscosity, filling connector, desired flow, oxygen sensitivity, dispensing orientation, reclosure, tamper evidence, and Carton Design.
Should samples be tested with water or the real liquid?
Water can support preliminary leak checks, but final compatibility, flow, aroma, migration, seal, and shelf-life work should use the actual product or a justified representative formulation.
What quality tests are important for bag-in-Box Packaging?
Relevant checks may include dimensions, film and seal verification, leak, pressure, burst, drop, vibration, fitment retention, dispensing, product compatibility, and migration evidence. Requirements should match application risk.
When should a customized bag-in-box package be revalidated?
Reassess changes to liquid formulation, film structure, thickness, adhesive, ink, fitment, sealing process, filling conditions, carton, production location, supplier, or distribution environment when they can affect performance.